## Overview of Thickness Scaling Challenges in CZT Planar Detectors
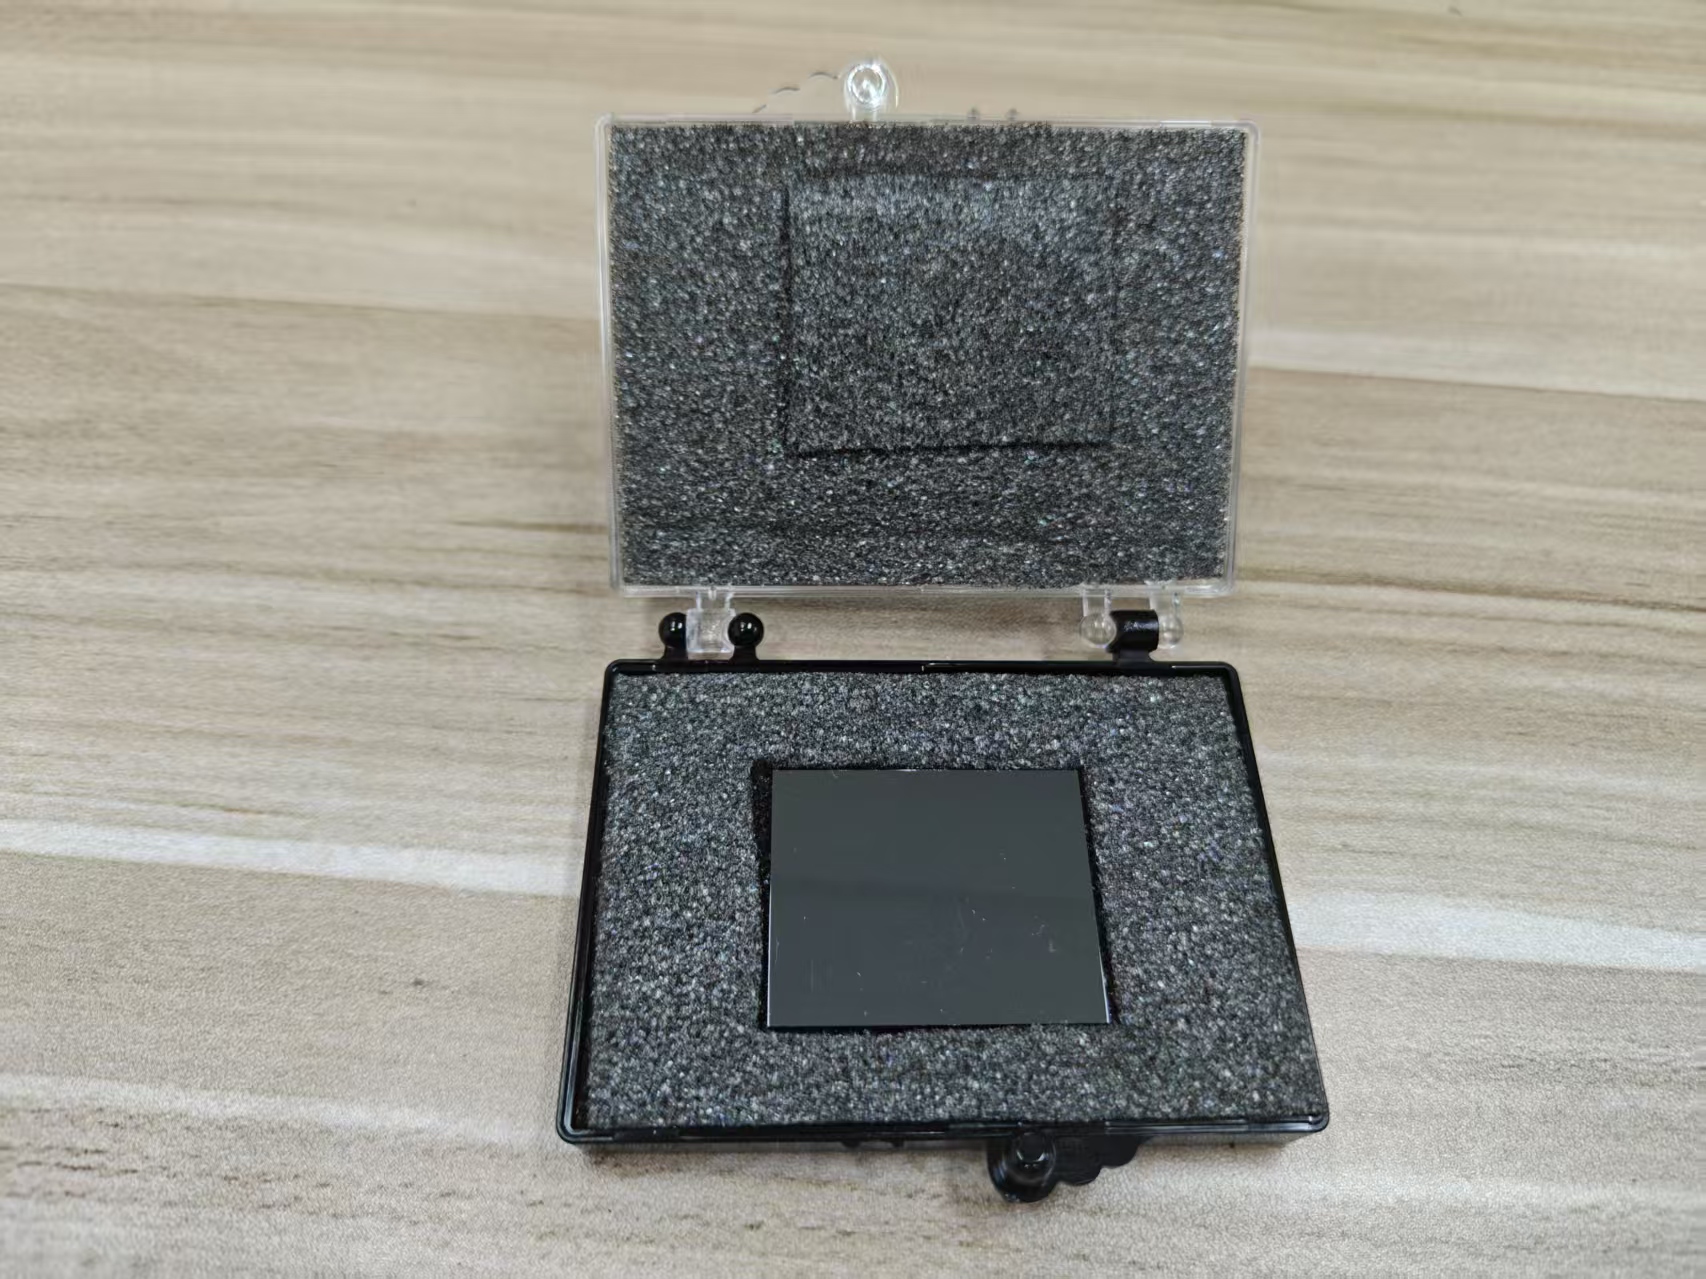
Scaling the thickness of CZT planar detectors beyond 10 mm introduces significant fabrication challenges that stem from the inherent limitations of cadmium zinc telluride crystal growth, mechanical properties, and surface processing techniques. Planar detectors rely on simple opposing electrodes to establish a uniform drift field across the crystal volume, making thickness directly proportional to stopping power for high-energy gamma rays. However, commercial CZT boules produced by the traveling-heater method or vertical Bridgman growth are typically optimized for slices of 2–10 mm, where uniformity is achievable. Thicker crystals demand larger growth runs, longer processing times, and more stringent controls to maintain high resistivity (>10^9 Ω·cm), low defect density, and uniform carrier transport properties. These issues manifest as reduced yield, increased leakage currents, non-uniform electric fields, and degraded spectroscopic performance, ultimately limiting the practical upper thickness for high-resolution planar detectors to around 15 mm in most production scenarios.
## Crystal Growth Limitations for Thicker Boules
Growing CZT crystals thicker than 10 mm requires extended growth periods in the traveling-heater method, where the molten zone moves slowly through the feed material to produce single-crystal ingots. Longer growth runs increase the probability of constitutional supercooling and interface instability, leading to polycrystalline regions or twin boundaries that render large sections unusable for detector fabrication. Maintaining a stable temperature gradient over the extended length of a thick boule is technically demanding; even small fluctuations (a few degrees Celsius) cause variations in solidification rate that promote secondary-phase formation. As a result, the usable single-crystal yield per boule drops sharply beyond 10–12 mm thickness, necessitating multiple growth attempts or post-growth selection of only the most uniform axial sections. This directly impacts production scalability, as thicker detectors cannot be reliably sliced from standard 50–100 mm diameter boules without encountering growth-induced defects that compromise bulk resistivity.
## Compositional Inhomogeneity and Zinc Segregation
Zinc segregation along the growth axis becomes pronounced in thicker crystals because the effective segregation coefficient of zinc in the CdTe matrix deviates from unity during solidification. In a 15 mm thick slice, the zinc fraction can vary by several atomic percent from one face to the other, causing corresponding gradients in bandgap (1.5–1.6 eV), resistivity, and carrier mobility-lifetime products. These axial inhomogeneities produce position-dependent electric field strengths under a fixed bias voltage, leading to non-uniform charge collection efficiency across the detector thickness. During fabrication, such gradients must be mapped and compensated by selective slicing and orientation, but the process reduces usable material yield and requires individual detector characterization rather than batch processing. In planar geometry, where the drift field spans the entire thickness, these variations cannot be locally corrected by electrode patterning, amplifying spectroscopic non-uniformity in the final device.
## Increased Defect Density and Precipitate Formation
Larger crystal volumes in thick detectors increase the statistical likelihood of incorporating tellurium inclusions and precipitates, whose density typically ranges from 10^3 to 10^5 cm^{-3} even in high-quality material. During extended growth of thick boules, the longer residence time in the molten zone allows more Te-rich droplets to nucleate and grow, especially near the tail end of the ingot. These inclusions act as trapping centers and local field distorters, but their impact is magnified in thick planar detectors because charge carriers must traverse greater distances, raising the probability of encountering a defect. Fabrication attempts to mitigate this through post-growth annealing are less effective in thicker material, where heat diffusion is slower and thermal gradients during annealing can themselves induce additional precipitates. Consequently, thicker detectors exhibit higher baseline trapping probabilities, necessitating more rigorous screening and rejection of defective slices before electrode processing.
## Mechanical Handling and Polishing Difficulties
CZT is mechanically brittle with a low fracture toughness, making the handling and polishing of slabs thicker than 10 mm prone to cracking, chipping, or warping. Thicker crystals have greater self-weight and thermal mass, increasing the risk of stress-induced fractures during cutting from the boule or during lapping and polishing operations. Achieving optical-flat parallelism (better than 1 μm across the entire face) on both sides of a thick wafer is challenging because differential thermal expansion during polishing generates bow or warp that exceeds acceptable limits for uniform electrode deposition. Conventional mechanical polishing must be followed by chemomechanical steps, yet thicker samples require longer processing times and more aggressive slurry removal, which can introduce subsurface damage layers extending tens of micrometers into the bulk. Any residual stress or micro-cracks propagate under subsequent high-voltage bias, creating leakage paths that degrade detector performance.
## Uniform Surface Preparation and Etching Issues
Chemical etching and passivation of both large faces of a thick crystal must be performed simultaneously and uniformly to minimize surface leakage and ensure low-noise operation. Beyond 10 mm thickness, diffusion-limited etchant transport in the thicker geometry leads to non-uniform removal rates between the center and edges of the wafer, resulting in surface roughness variations or residual tellurium-rich layers that elevate inter-face conductivity. Achieving stoichiometric surfaces free of oxides or dangling bonds across the entire area requires precise control of etchant concentration, temperature, and agitation, yet thicker samples exacerbate boundary-layer effects and make it harder to prevent re-oxidation during rinsing and drying. These surface non-uniformities directly translate into higher leakage currents and position-dependent noise when electrodes are applied, limiting the spectroscopic resolution achievable in planar detectors.
## Electrode Deposition and Contact Uniformity Problems
Electroless gold deposition, the standard contact method for CZT planar detectors, becomes increasingly difficult to control uniformly over the larger surface area and greater edge-to-center distance of thick crystals. Deposition rate variations caused by local concentration gradients in the plating bath produce thickness non-uniformities or dendritic growth, leading to contact resistivity differences across the detector face. In thicker devices, the higher bias voltages required (several hundred volts) amplify any contact non-ohmic behavior, causing injection currents or breakdown at localized high-field spots. Mechanical stress from the thicker crystal during handling can also cause micro-delamination of the metal layer, creating dead zones or high-leakage paths. Achieving ohmic or quasi-ohmic contacts with consistent barrier heights on both faces simultaneously is thus more demanding, often requiring additional passivation layers or multi-step deposition processes that increase fabrication complexity and cost.
## Passivation Layer Application on Larger Surfaces
Surface passivation, typically using aluminum oxide or chemical oxide/sulfide layers, must provide high resistivity (>10^12 Ω·cm) and low interface trap density over the entire active area of a thick detector. Scaling thickness increases the surface-to-volume ratio challenge because the passivation must be conformal and pinhole-free across larger lateral dimensions while accommodating the greater edge perimeter. Plasma-enhanced or atomic-layer deposition techniques suffer from reduced precursor penetration and film density variations in thicker geometries, leading to incomplete coverage near edges or corners. Any defects in the passivation layer create surface conduction channels that shunt the bulk field, elevating leakage currents disproportionately in thick detectors where bulk resistance is already higher. Uniform passivation is therefore harder to achieve without specialized reactor designs or multiple deposition cycles, further reducing process yield.
## Bias Voltage Requirements and High-Voltage Stability Issues
Thicker planar detectors require proportionally higher bias voltages to maintain adequate drift fields (typically >1000 V for 15 mm thickness), increasing the risk of dielectric breakdown at material imperfections or surface edges. Fabrication-induced micro-cracks, inclusions, or non-uniform resistivity create localized high-field regions that trigger avalanche or surface flashover during high-voltage testing. Encapsulation and edge passivation must therefore be scaled accordingly, yet thicker crystals complicate uniform potting or guard-ring application, leaving vulnerable paths for corona discharge or catastrophic failure. These high-voltage issues necessitate more rigorous electrical screening and often result in lower overall device yield compared with thinner counterparts.
## Overall Yield Reduction and Cost Implications
The cumulative effect of these fabrication challenges leads to a sharp drop in usable detector yield when thickness exceeds 10 mm. Crystal growth yield, mechanical yield, surface processing yield, and final electrical yield all decline, driving up per-detector cost and limiting commercial availability of thick planar CZT devices. Batch processing becomes inefficient because each thick slice must be individually qualified, and defective regions cannot be easily trimmed without wasting material. These issues constrain the practical application of thick planar detectors to specialized high-efficiency needs, where the benefits of increased stopping power must be balanced against the higher fabrication risk and expense. Advances in growth technology and automated processing continue to mitigate some limitations, but scaling beyond 10–12 mm remains a significant engineering hurdle for high-performance CZT planar detector production.
CdZnTe Association (CdZnTe.com)
https://www.cdznte.com/blog/what-fabrication-issues-arise-when-scaling-the-thickness-of-a-czt-planar-detector-beyond-10-mm.html